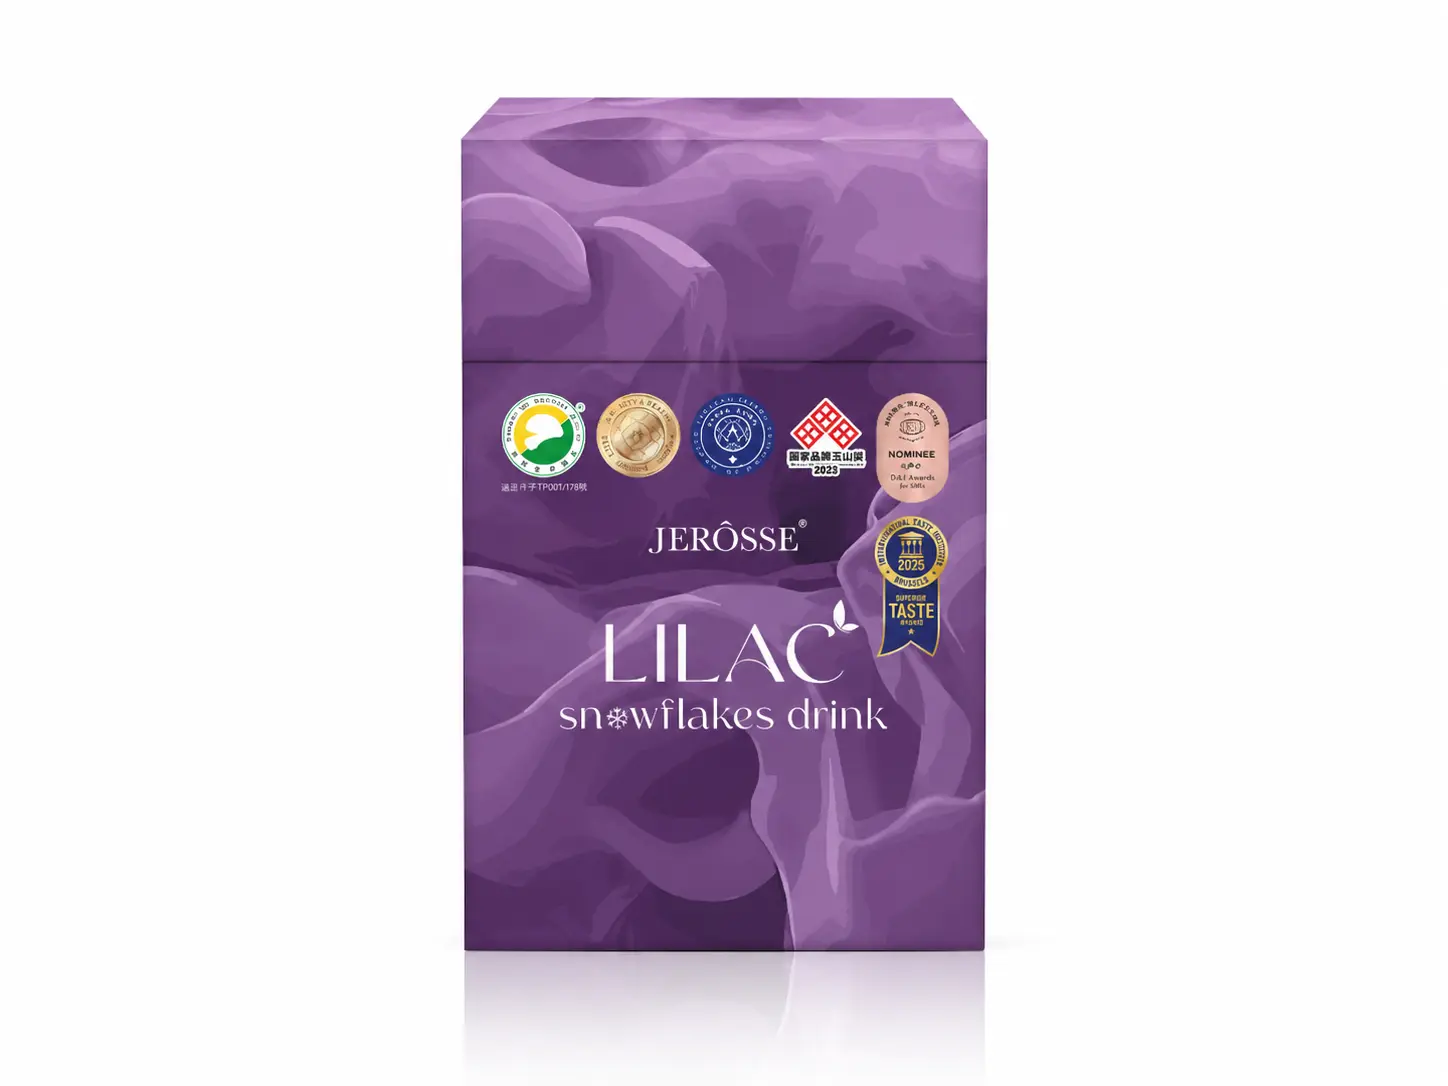
Lilac Snowflake Drink is a powdered health beverage designed to support metabolism, health maintenance, and daily nutritional supplementation. The formula features Reducose®, a patented mulberry leaf extract supported by Innovate UK/UKRI research, combined with Cellbeery®, Korean pumpkin extract, and other plant-derived ingredients. It is suitable for daily body management, metabolic regulation, and post-GLP-1 weight management nutritional support.
The product combines three key ingredients: mulberry leaf extract for health maintenance, physiological regulation, and metabolic support; wild cherry extract, rich in phytochemicals and anthocyanins, for beauty support; and Korean pumpkin extract to help maintain normal water metabolism and body balance. With a refreshing cranberry flavor, individual powder packets, color-changing technology, and a reverse microbubble floating effect, it offers both functional value and an enjoyable drinking experience. The product is zero fat and contains no preservatives, bleaching agents, binders, artificial colors, or bactericides.
Lilac Snowflake Drink is supported by multiple international patents and certifications, insured with NT$600 million product liability insurance.
Awarded the Monde selection Awards
Awarded the National of safety and quality Awards
Awarded the National Brand Yushan Award
Awarded the Michelin iTQi International Taste Excellence Medal
Awarded the A.A. Taste Awards for Global Pure Flavor
Cranberry powder pack: Instant blueberry juice powder (sugar, maltodextrin, blueberry juice concentrate, citric acid, sodium citrate, flavors, grape skin coloring, gardenia blue coloring), patented corn-derived soluble dietary fiber Fibryxa® (isomaltodextrin), instant cranberry juice powder (sugar, maltodextrin, cranberry juice concentrate, flavors, citric acid, sodium citrate, red beet juice, annatto coloring, gardenia blue coloring), potassium bicarbonate, citric acid anhydrous, pumpkin extract (pumpkin extract, maltodextrin), sodium bicarbonate, patented mulberry leaf extract Reducose® (mulberry leaf extract, maltodextrin, L-leucine), flavor compound (lactose, propylene glycol, silicon dioxide, flavors, β-cyclodextrin, water), patented aronia extract (aronia extract, maltodextrin), sucralose.
White fungus pack: White fungus, sweetener (D-sorbitol solution).
Each serving contains 200mg of Reducose® mulberry leaf extract.
Our products are manufactured in a world-class, ISO 22000-certified facility. To ensure safety, stability, and efficacy, our professional QA/QC teams oversee a complete quality control system across three stages: Incoming Quality Control, In-Process Quality Control, and Final Quality Control. At the incoming stage, all key raw materials and packaging undergo batch-by-batch inspections to meet strict specifications. During production, we monitor Critical Control Points (CCPs) and Operational Prerequisite Programs (OPRPs). By controlling temperature, humidity, time, and blending uniformity, we ensure consistent batch quality. Before shipment, finished products must pass hygiene, safety, and efficacy testing.
Hygiene & Safety Compliance Rate Batch-by-batch release testing for regulated microorganisms.
Target: 100% — Zero tolerance for safety deviations.
Active Ingredient Compliance Rate Stability testing ensures active ingredients remain aligned with label claims throughout shelf life.
Target: ≥ 98% — Allowing minor natural variations while meeting regulatory limits.
Finished Product Appearance & Physical Compliance Rate Random finished-product sampling checks appearance, flavor, weight, and packaging integrity.
Target: ≥ 99% — Ensuring a consistent, high-quality user experience across every batch.
3 regulated microorganisms (Staphylococcus aureus, Salmonella spp., and Listeria monocytogenes), 5 heavy metals, 502 pesticide residues, and 365 chemicals for clinical use
Incoming & In-Process Risk Control At the source, we apply a dual safety system combining supplier management and independent testing. Every batch must provide a Certificate of Analysis (COA), while additional voluntary safety tests are scheduled annually based on product characteristics and higher standards, such as infant food regulations. During production, QA teams conduct frequent floor audits and monitor key control data. If any value approaches a critical limit, an early warning is triggered to prevent defects before they occur.
Finished Product Warehousing & Post-Market Risk Control Before shipment, finished products are stored in a dedicated warehouse with strict temperature, humidity, and pest controls to maintain quality stability. After shipping, our traceability system monitors every batch beyond standard logistics tracking. QA teams continue post-market surveillance until one month after the product’s expiration date, ensuring safety and efficacy throughout the entire shelf life.
Emergency Risk Control For major quality or safety incidents, a dedicated Product Safety Response Team is ready to act within 24 hours. The team rapidly coordinates cross-functional resources, performs risk assessments, traces data to the source, and executes precautionary recalls and Corrective and Preventive Actions (CAPA) when needed, protecting consumer safety and brand trust.