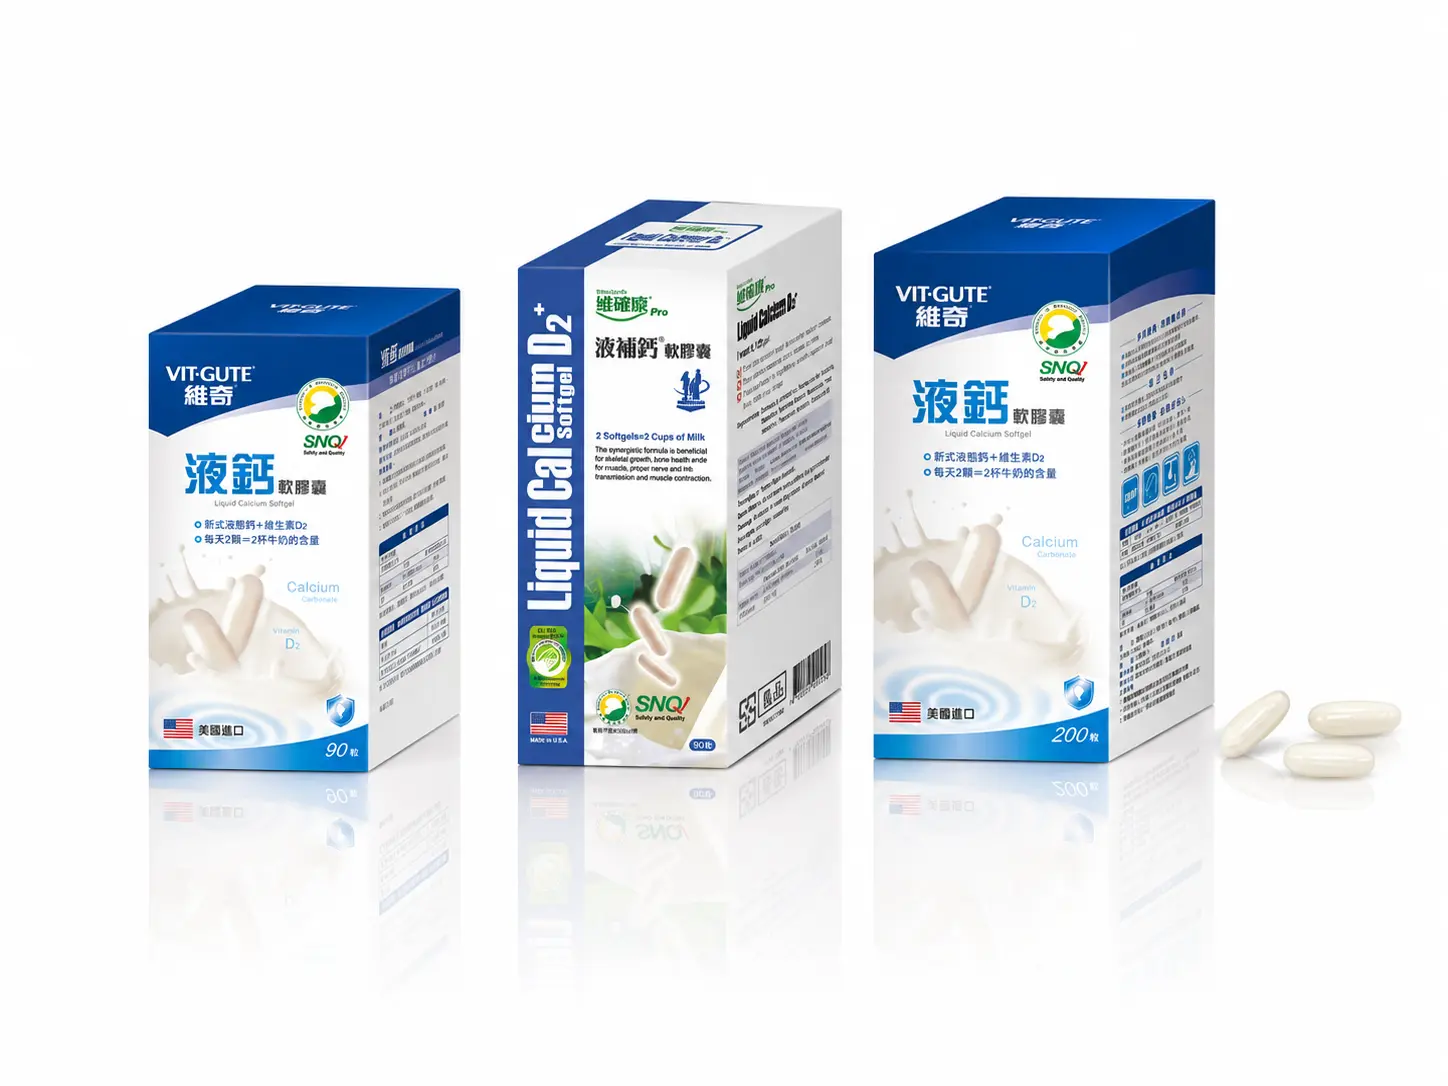
Highly Absorbable: Micronized for rapid disintegration and absorption.
Safe and Reliable: Compliant with the U.S. National Institutes of Health; each tablet contains 350mg of pure calcium.
Naturally Contains Vitamin D2 and mineral calcium carbonate.
Rich in Calcium: Each 2 tablets contain the equivalent calcium of 700ml of milk.
Healthier: Calcium + Vitamin D2 maintains healthy bones and teeth, assists in normal muscle contraction and nerve function.
Calcium carbonate, soybean oil, gelatin, glycerin, purified water, beeswax, soybean lecithin, titanium dioxide, corn oil, vitamin D2
Calcium 350mg/capsule; Vitamin D 2.5 mcg (100 IU)/capsule
This product is manufactured under a comprehensive quality management system covering raw materials, production processes, semi-finished products, and finished goods. All raw materials and packaging components undergo incoming inspection and document verification (COA) prior to production use. During manufacturing, critical parameters such as softgel weight, seal integrity, appearance, and processing conditions are continuously monitored to ensure product consistency and stability. Before release, each batch is subject to final quality inspection and QA review. Complete batch and testing records are maintained to ensure full traceability. In addition, data-driven quality management is implemented through batch qualification monitoring, process deviation analysis, and trend evaluation to support continuous improvement and long-term product quality stability.
Product safety and quality are ensured through both internal quality controls and regular third-party laboratory testing. Testing is conducted in accordance with applicable regulations and recognized analytical standards to verify product safety and compliance. Routine testing items include microbiological analysis (total plate count, coliforms, yeast and mold), heavy metals (lead, arsenic, cadmium, mercury), and other necessary safety-related parameters. A multi-layer quality assurance system is implemented throughout raw material sourcing, manufacturing, and finished product release. Complete testing records and Certificates of Analysis (COA) are maintained to ensure product safety, quality consistency, and traceability.
This product is managed under a comprehensive risk management system based on ISO 22000 and HACCP principles, covering raw materials, manufacturing processes, finished products, and post-market monitoring. Raw material controls include supplier qualification, incoming inspection, and risk assessment. During production, critical control points (CCPs), equipment hygiene, personnel practices, and environmental conditions are continuously monitored to minimize contamination and quality risks. Finished products are released only after quality verification and approval, with full batch traceability and deviation handling procedures in place. Post-market surveillance activities, including complaint handling, incident reporting, and CAPA implementation, are conducted to continuously improve the food safety management system and ensure product quality and consumer safety.