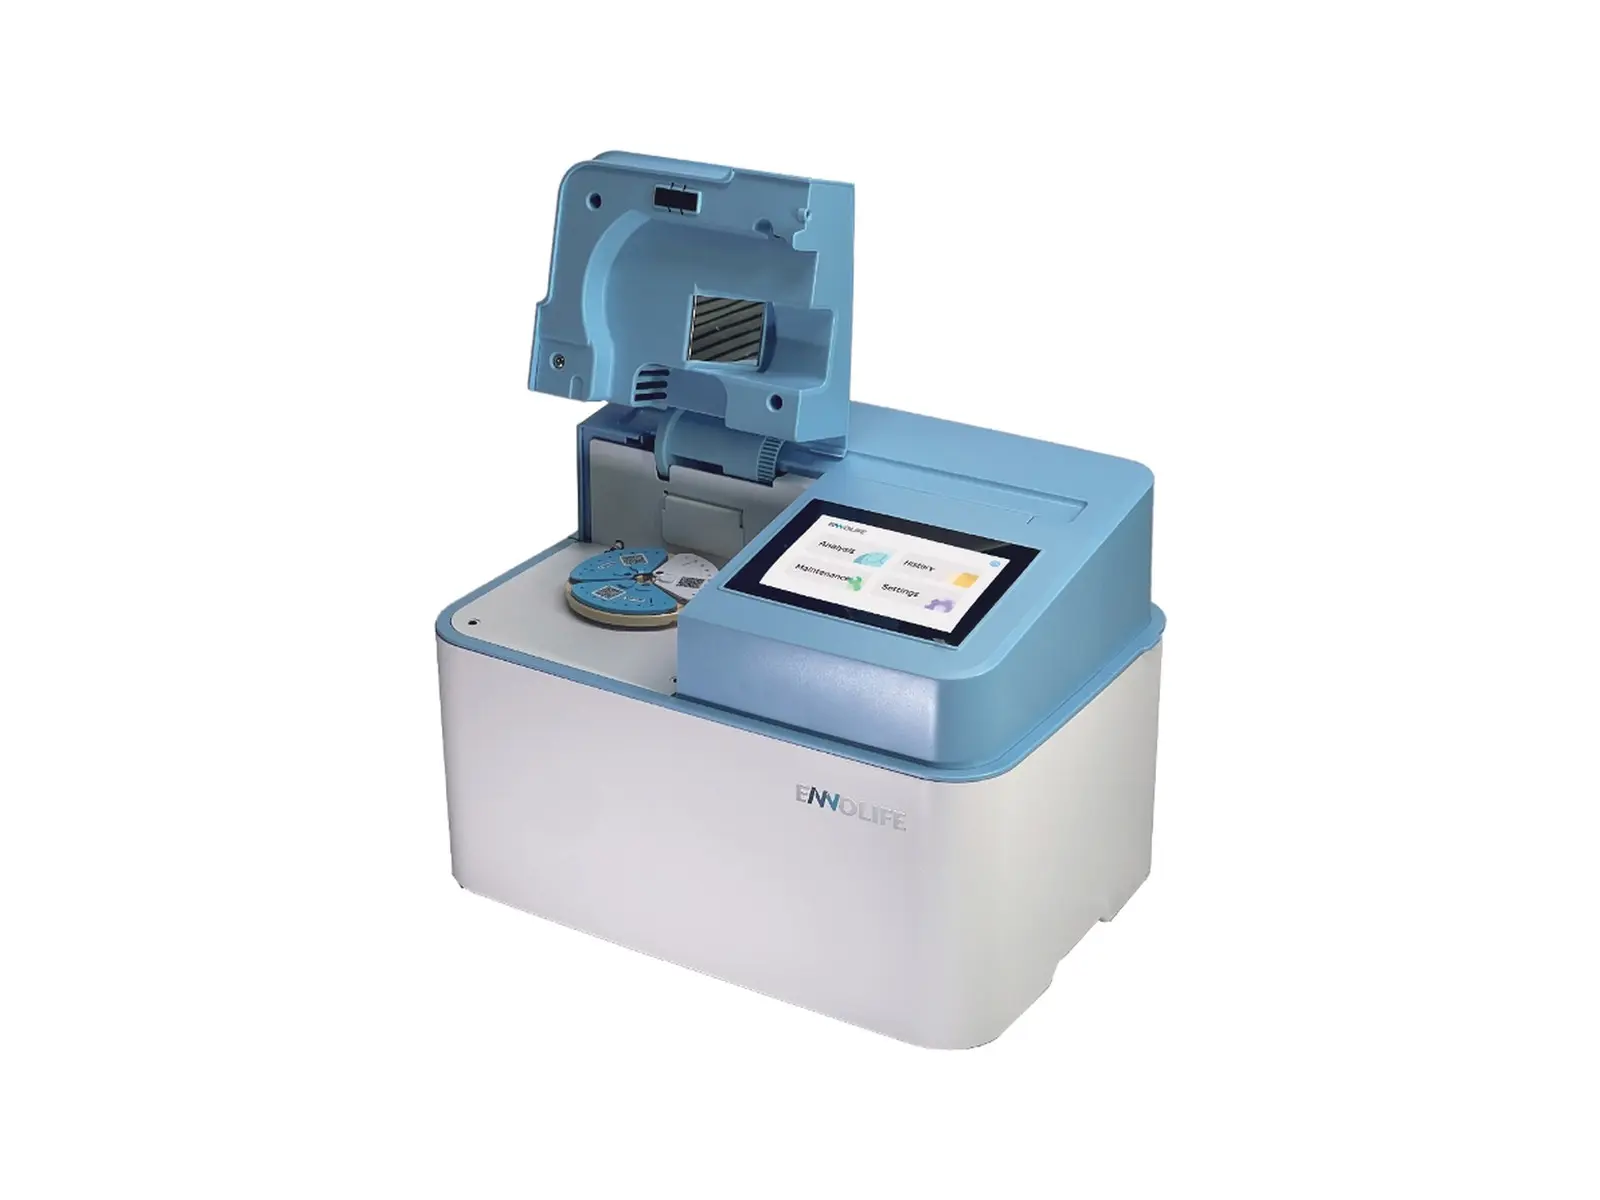
ENNOLIFE Clinical Chemistry Analyzer Powered by advanced full-spectrum analysis technology, the ENNOLIFE Clinical Chemistry Analyzer is specifically designed for In-Vitro Diagnostic (IVD) applications. Using only a small amount of serum, plasma, whole blood, or urine, it can rapidly detect concentrations of various biomarkers, delivering real-time and reliable diagnostic results. By integrating microfluidic technology with a user-friendly design, it is well-suited for a wide range of point-of-care settings such as clinics, nursing centers, ambulances, schools, corporate wellness stations, and remote areas. This makes it an ideal tool for enhancing the efficiency of primary care and personal health management.
Enolife Clinical Chemistry Analyzer(Non-sterile)
ProtectLife International Biomedical Inc.
The ENNOLIFE Clinical Chemistry Analyzer strictly adheres to ISO 13485:2016, Taiwan TFDA QMS guidelines, and EU medical device regulations through comprehensive Design Verification and Validation protocols. 1. Development & Production Validation Efficient Micro-Sample Testing: The validated core multi-functional optical platform pairs with specialized reagent discs to deliver precise results using just 60 μL of blood within 20 minutes. Reproducibility & Data Integrity: Process validation and inline monitoring ensure high batch-to-batch reproducibility. All quality system software undergoes strict confirmation to guarantee data accuracy and traceability. 2. Performance Testing & Specifications The optical system passes rigorous linearity validation and inspection protocols: Stray Light Suppression: Maintains excellent measured values even under high absorbance, demonstrating superior optical hardware quality. Absorbance Linearity & Accuracy: Proven exceptional linear correlation across multi-concentration gradients within each wavelength's dynamic range, supporting high-standard clinical testing of up to 17 simultaneous markers in a single run. 3. Third-Party Safety Certifications IVD Compliance: Verified by accredited third-party laboratories to meet international In Vitro Diagnostic (IVD) medical device safety and performance standards. Biosafety Assurance: Fully validated microfluidic paths and operation methods ensure optimal biosafety for both personnel and environments.
The Company has established a comprehensive quality management system in accordance with medical device quality management requirements. The quality control process covers all stages including incoming material inspection, in-process control, semi-finished product inspection, finished product inspection, and shipment release management to ensure product stability and consistency. For raw material management, all critical raw materials and reagents are subject to supplier qualification and incoming inspection procedures. Inspection items include appearance, specifications, functionality, and batch consistency verification. Only materials that meet the established specifications are approved for production use. For process management, critical process parameters (CPP) and critical quality attributes (CQA) are monitored and controlled throughout the manufacturing process. Monitoring items include coefficient of variation (CV), resolution, stability, and batch-to-batch variation analysis. Standardized SOPs and production records are implemented to ensure process control and full traceability. Semi-finished products and finished products are inspected and verified according to established quality specifications, including tests for accuracy, reproducibility, consistency, and compliance rate, to ensure conformity with design outputs and regulatory requirements. All finished products are reviewed and approved by the Quality Assurance unit prior to shipment release.
The Company has incorporated a risk management mechanism into its quality management system. Risk identification, assessment, and control are implemented throughout all stages, including incoming material inspection, process control, finished product inspection, and post-market surveillance, in order to prevent product failure, reduce the occurrence of abnormalities, and minimize potential impacts on users or patients. In addition to quality control measures such as incoming inspection, self-inspection, and product release procedures, the Company has established management mechanisms for abnormal event reporting, corrective and preventive actions (CAPA), product traceability, and customer feedback monitoring to continuously monitor and improve potential risks. After product commercialization, the Company continuously conducts market surveillance and customer feedback collection activities, including complaint handling, adverse event monitoring, product usage analysis, and periodic quality reviews. Risk assessments and improvement actions are implemented based on monitoring results to ensure that product quality, safety, and effectiveness are maintained throughout the entire product lifecycle and remain compliant with applicable medical device regulations and quality management requirements.
The Company has established a post-market surveillance system to continuously monitor product quality, safety, and use, ensuring compliance with applicable medical device regulations throughout the product lifecycle. Post-market activities include safety monitoring, customer feedback collection, complaint and adverse event handling, and product performance analysis, supported by periodic quality reviews and risk assessments. For software or system products, the Company maintains maintenance and version control procedures, including updates, issue correction, compatibility checks, and verification to ensure stability and safety. In the event of quality issues or potential risks, the Company promptly initiates crisis management and reporting procedures. Cross-functional teams conduct investigation, root cause analysis, and risk assessment, followed by corrective and preventive actions (CAPA), product traceability, and, where necessary, market notification or recall. Through continuous monitoring and improvement, the Company is committed to maintaining product quality, safety, and effectiveness.