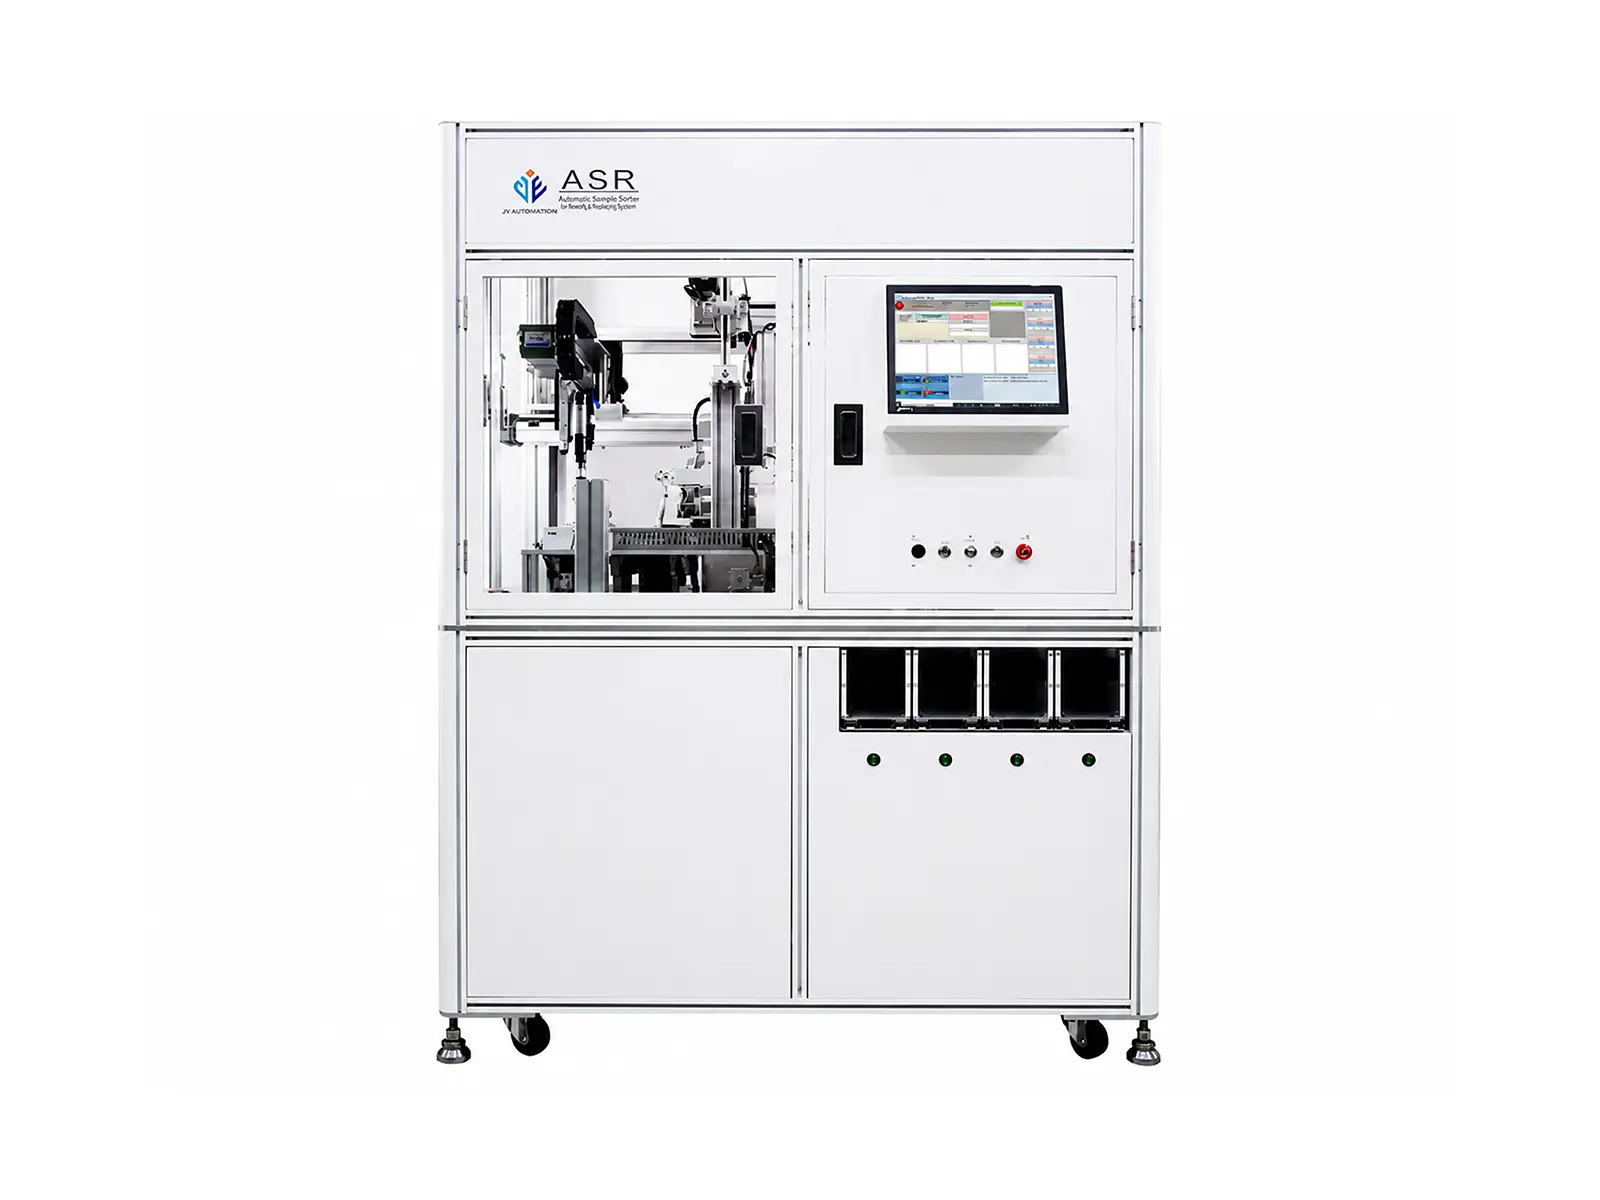
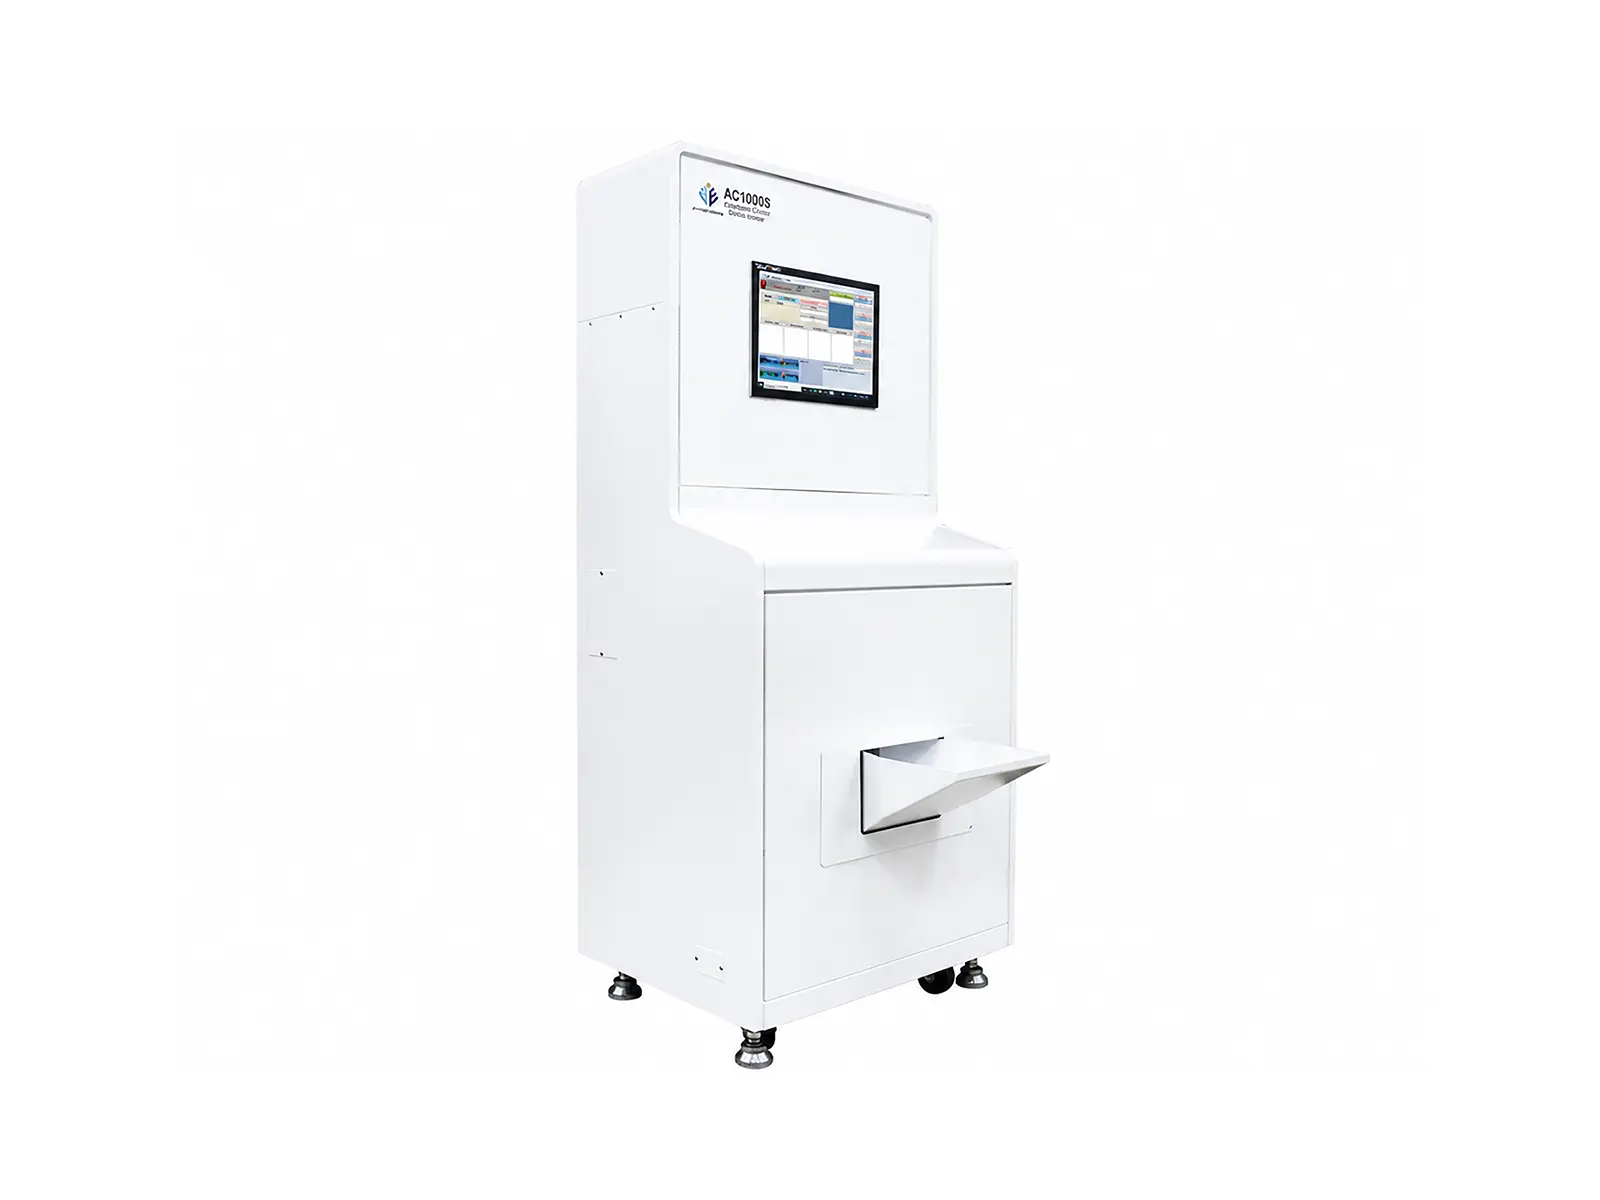
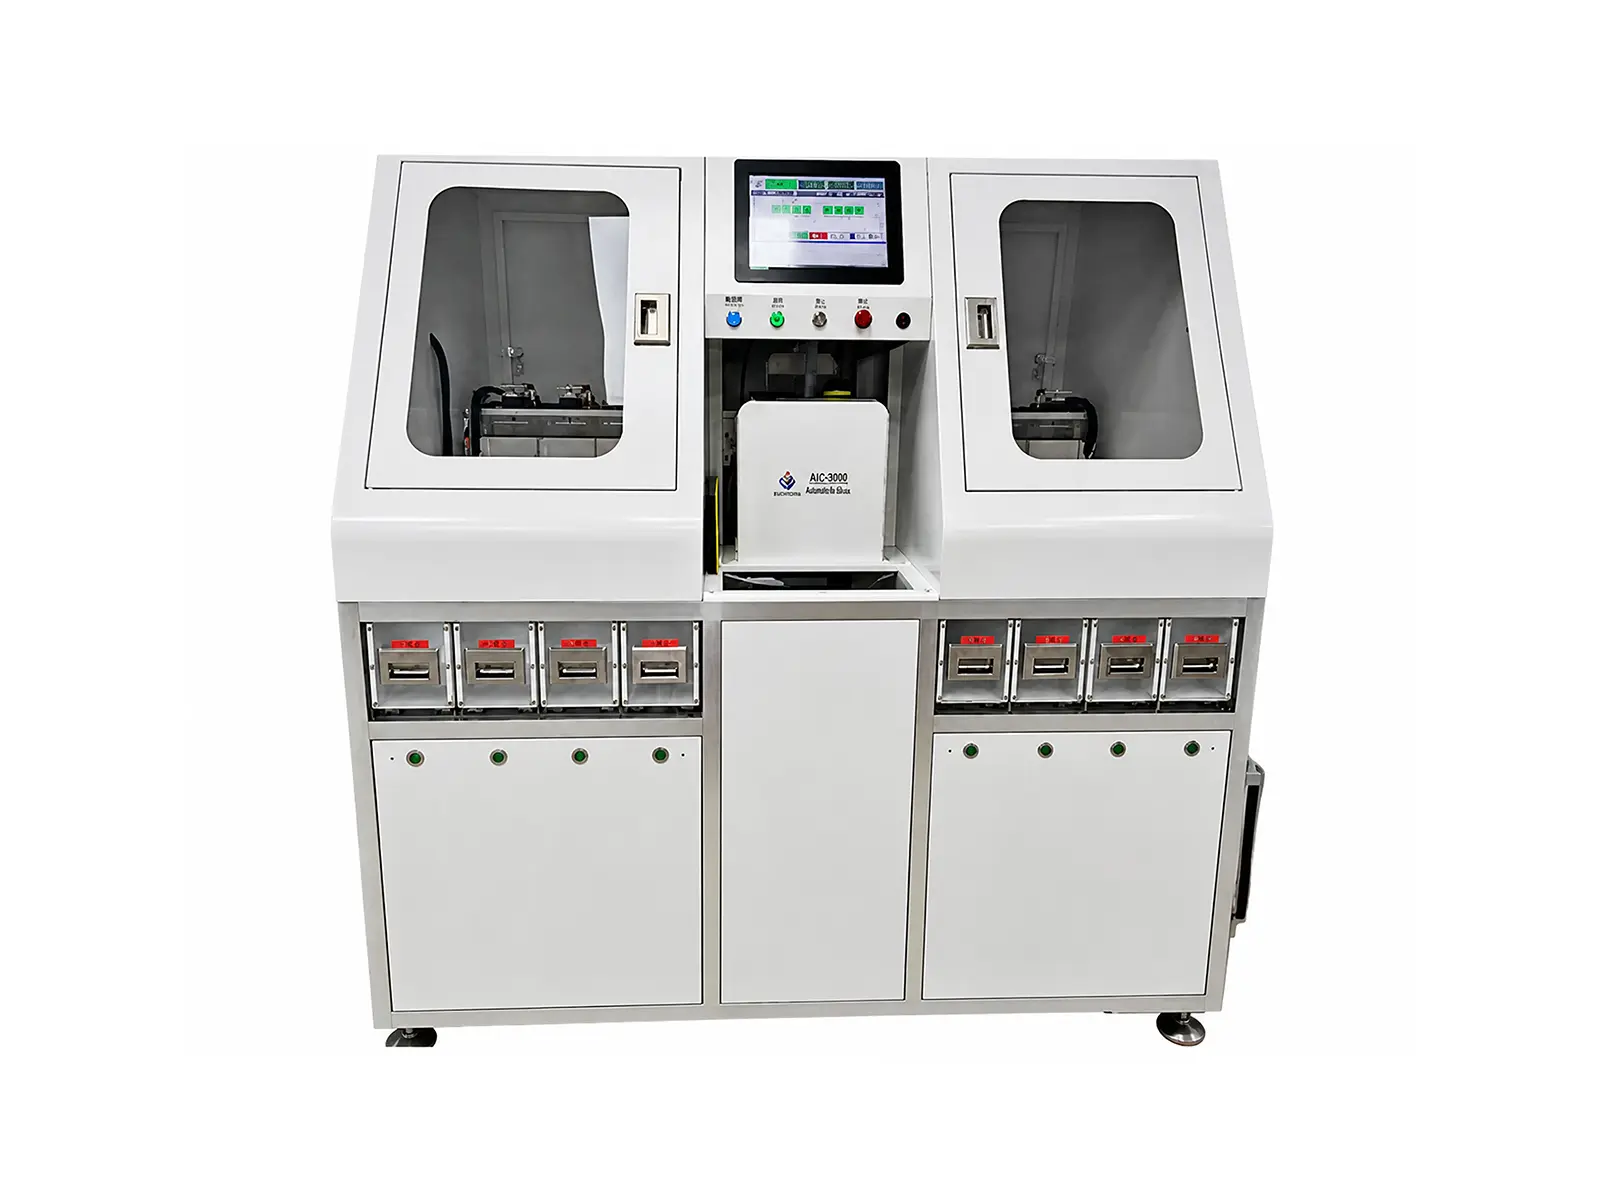
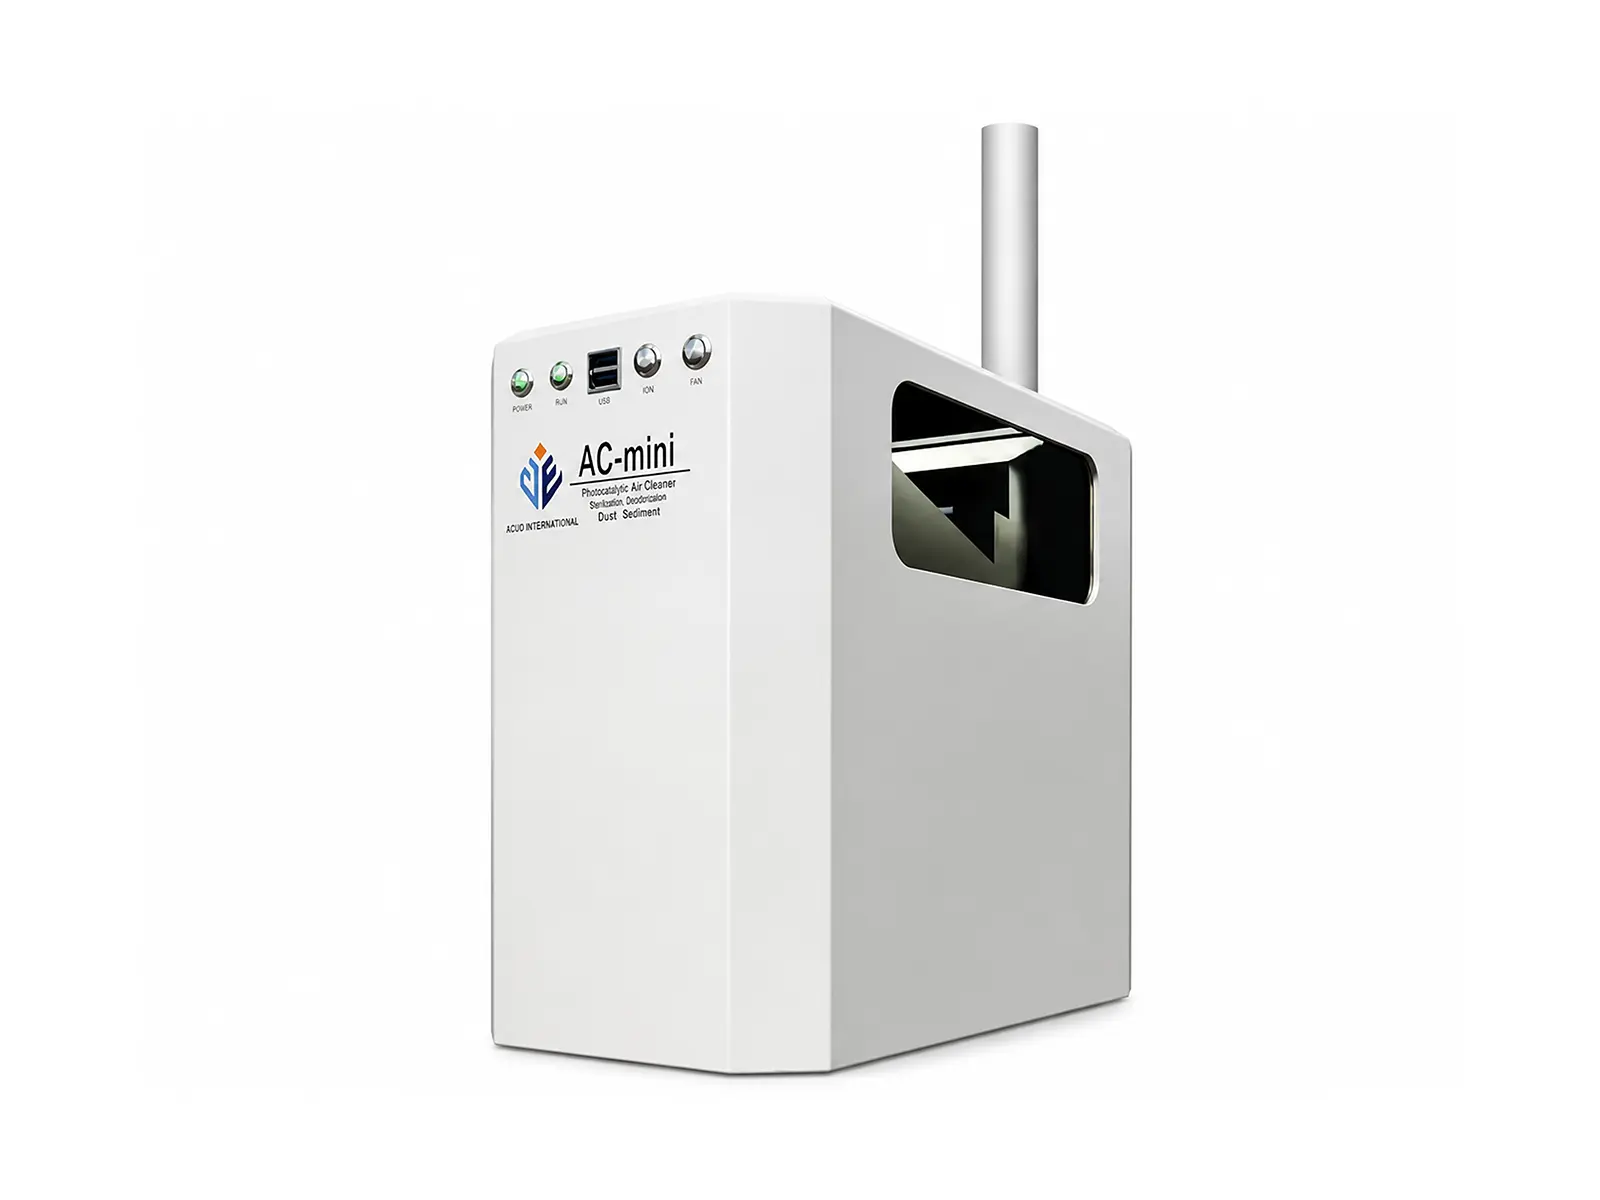
The AC1000 Smart Specimen Transportation System is designed to make specimen transportation faster, safer, and smarter. Powered by our three patented Positive-Negative Pressure Switching Technology, patented pressure-release and deceleration mechanisms, the AC1000 Series enables high-speed specimen transportation while minimizing impact forces, reducing the risk of tube damage, specimen loss, and hemolysis. The system supports long-distance transportation across departments, floors, and buildings. Integrated barcode tracking, automatic receipt logging, and real-time monitoring provide complete specimen traceability from collection to analysis. The system helps reduce turnaround time (TAT), lower labor costs, minimize human errors, and enhance patient safety. Reducing manual handling, minimizing transportation risks, and improving laboratory efficiency. Designed for high throughput, reliability, and scalability, the AC1000 Series seamlessly integrates with Laboratory Information Systems (LIS), the system supports laboratory automation and healthcare digital transformation. Widely adopted by medical centers, regional hospitals, emergency departments, and clinical laboratories, By combining innovative technology, intelligent logistics management, and full specimen traceability, the AC1000 Series enables healthcare organizations to improve operational efficiency and build smarter laboratories for the future.
Our Smart Specimen Transportation System is designed and manufactured under a rigorous quality management framework to ensure exceptional safety, reliability, and performance. The system is ISO 9001:2015 certified, protected by six invention patents, and recognized with the SNQ National Quality Award Bronze Medal. Comprehensive validation and performance testing were conducted during product development using various types of vacuum blood collection tubes. Critical parameters, including transport distance, operating pressure, tube compatibility, and deceleration control, were thoroughly verified. Testing demonstrated 100% specimen tube integrity with no cap loss or tube collision, while achieving a throughput of more than 1,000 specimens per hour over a 100-meter transport distance. Based on nearly 990,000 real-world specimen transports in hospital environments, the measured hemolysis rate remained below 1%, demonstrating superior specimen protection and diagnostic reliability. The system has also been validated for long-distance and multi-floor transportation, including successful vertical transport tests at heights of 30 and 75 meters. Designed for high-volume healthcare environments, the AC1000 Series provides full specimen traceability, operational efficiency, and dependable performance, helping hospitals accelerate laboratory automation, digital transformation, and smarter specimen logistics management.
Manufacturer: JU YUH Enterprise Co., Ltd.
Our Smart Specimen Transportation System is designed and manufactured under a rigorous quality management framework to ensure exceptional safety, reliability, and performance. The system is ISO 9001:2015 certified, protected by six invention patents, and recognized with the SNQ National Quality Award Bronze Medal. Comprehensive validation and performance testing were conducted during product development using various types of vacuum blood collection tubes. Critical parameters, including transport distance, operating pressure, tube compatibility, and deceleration control, were thoroughly verified. Testing demonstrated 100% specimen tube integrity with no cap loss or tube collision, while achieving a throughput of more than 1,000 specimens per hour over a 100-meter transport distance. Based on nearly 990,000 real-world specimen transports in hospital environments, the measured hemolysis rate remained below 1%, demonstrating superior specimen protection and diagnostic reliability. The system has also been validated for long-distance and multi-floor transportation, including successful vertical transport tests at heights of 30 and 75 meters. Designed for high-volume healthcare environments, the AC1000 Series provides full specimen traceability, operational efficiency, and dependable performance, helping hospitals accelerate laboratory automation, digital transformation, and smarter specimen logistics management.
Guided by our ISO 9001:2015 QMS, we have established a comprehensive quality assurance framework covering the entire product lifecycle, including design and development, supply chain management, procurement, manufacturing, assembly, testing, delivery, installation, and after-sales service. All critical components—including sensors, pneumatic devices, control modules, and communication equipment—undergo strict incoming quality inspections. Each component is verified and compliance before entering production. During manufacturing, products are assembled and tested in accordance with SOPs and engineering control requirements. Key performance parameters such as pressure control, transport speed, positioning accuracy, barcode recognition, communication functions, and safety protection mechanisms are inspected and recorded. All critical process data are managed to ensure product consistency, traceability, and long-term reliability. Before shipment, every system undergoes comprehensive validation, including full functional testing, long-duration operational testing, abnormal condition simulations, and transport performance verification. After installation, Site Acceptance Testing and operator training are conducted to ensure optimal system performance in the customer environment. We monitor key performance indicators , including MTTR , MTBF , equipment availability, customer-reported incidents. These metrics are regularly reviewed to drive ongoing improvements.
We have established a risk management system covering the entire product lifecycle, including incoming materials, manufacturing, installation, operation, and after-sales service. Through preventive controls, continuous monitoring, and corrective actions. we proactively minimize operational and specimen transportation risks. Critical components undergo supplier qualification and incoming quality inspections to verify performance, functionality, and reliability. During manufacturing, in-process inspections and functional testing ensure consistent product quality and stable system performance. The system incorporates multiple safety features, including a closed-loop transportation pipeline, patented positive-negative pressure switching technology, barcode-based specimen tracking, automatic receipt logging, and real-time alarm notifications. These features reduce the risk of specimen loss, and human error while providing complete traceability throughout the transportation process. To address potential risks such as specimen damage, hemolysis, and system downtime. We have implemented standardized response procedures and risk control measures. These include impact-reduction and deceleration designs, automatic fault notifications, data backup systems, user access controls, and software validation protocols. All software upgrades are validated through simulation testing before deployment.
We have established a comprehensive post-market surveillance program to monitor the safety, reliability, and operational performance of our systems in real-world healthcare environments. We utilizes barcode identification integrated with Laboratory Information Systems (LIS) to ensure specimen accuracy and data integrity. All transportation, receiving, and sorting records are automatically stored in the system database with time stamps and receipt logs, providing complete traceability throughout the specimen handling process. To maximize operational reliability, the system features real-time monitoring, self-diagnostics, alarm notifications, overload detection, and emergency stop functions. These capabilities enable rapid identification and resolution of potential issues, minimizing downtime and ensuring uninterrupted laboratory operations. All installed systems are included in scheduled maintenance and inspection programs, with preventive maintenance strategies designed to optimize performance and reduce equipment failure risks. For software management, we maintain a robust version control and validation process, including functional verification, simulation testing, and controlled software deployment. Critical data are regularly backed up, while user access controls help protect system integrity and operational continuity. Today, our systems are successfully deployed in leading medical centers, regional hospitals, and international healthcare markets.
None
1. Negative pressure delivery system China National Intellectual Property Administration, Invention Patent Number ZL 2020 2 0849267.9
Circuit system using negative pressure transmission (AC 1000 First generation) China National Intellectual Property Administration, Invention Patent Number ZL 2020 1 0429534. 1
Circuit system using negative pressure transmission Intellectual Property Office, Ministry of Economic Affairs, R.O.C. Invention Number I733335
Test tube sorting device and the negative pressure transport circuit system utilizing the test tube sorting device Intellectual Property Office, Ministry of Economic Affairs, R.O.C. Patent Number M621659
Negative pressure delivery system Intellectual Property Office, Ministry of Economic Affairs, R.O.C. Invention Number I820768
Negative pressure delivery system Philippines Bureau of Patents. Patent NO.:1/2023/050292 B1 Intellectual Property Office of the Philippines Bureau of Patents
Positive & Negative Pressure switching device Intellectual Property Office, Ministry of Economic Affairs, R.O.C. Invention Number I909995
PRESSURE RELIEF STRUCTURE FOR CONVEYING ITEMS Intellectual Property Office, Ministry of Economic Affairs, R.O.C. Patent Number I926687
Pressure relief device Intellectual Property Office, Ministry of Economic Affairs, R.O.C Patent Number M672869